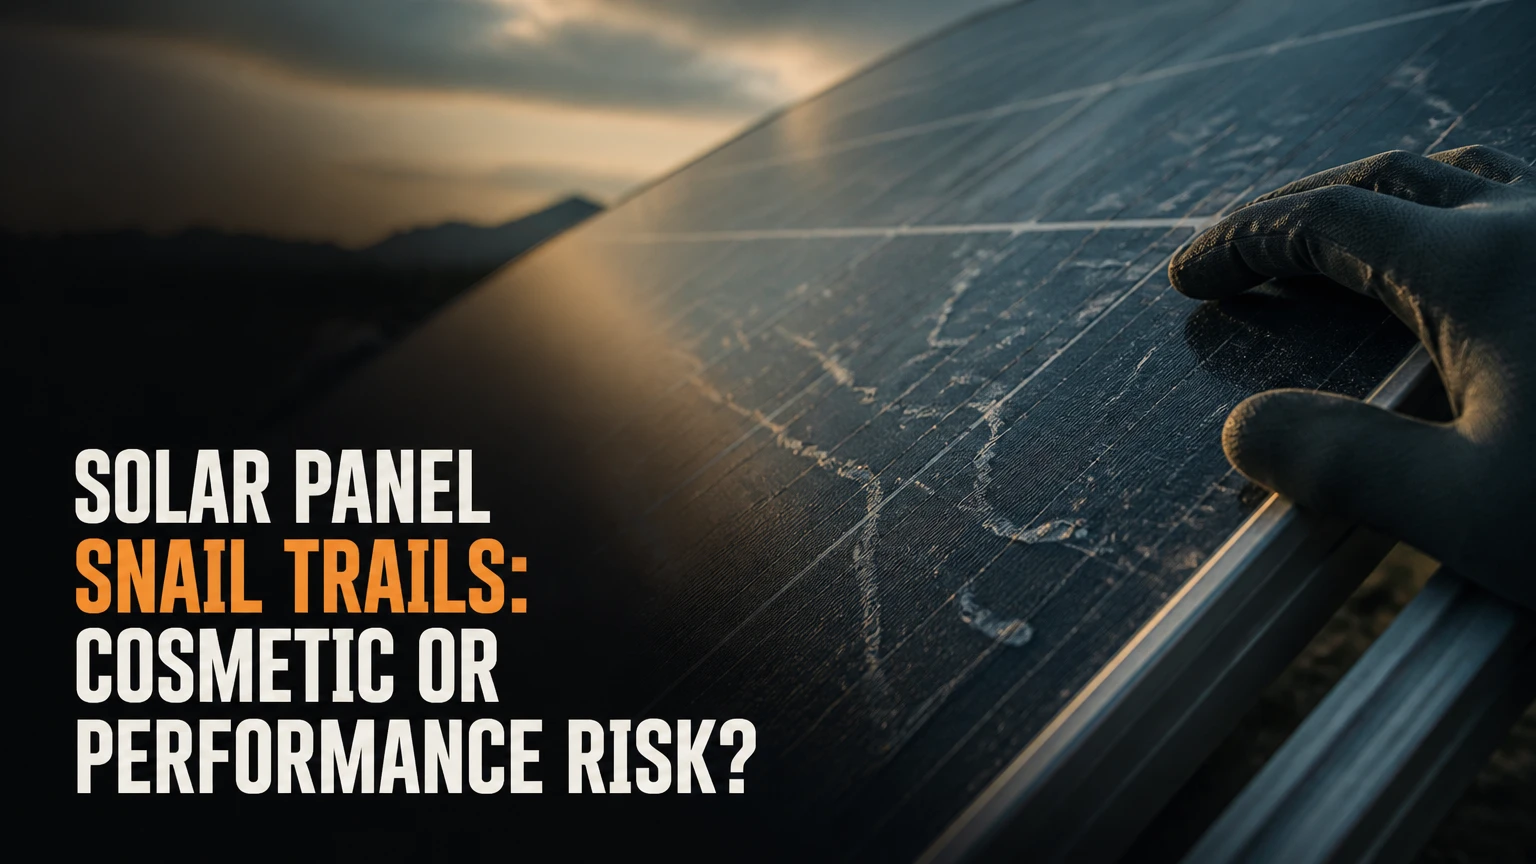
Solar panel snail trails are dark, branching or linear marks within a laminated crystalline-silicon module. They are often cosmetic at first, but they can indicate cell microcracking, moisture-related corrosion, or inactive cell areas, so appearance alone cannot establish performance risk. Confirm the condition with production data and targeted electrical or thermal testing.
Key Facts at a Glance
- Solar panel snail trails usually lie beneath the front glass and inside the encapsulant, not on the washable surface.
- A visible trail does not prove a specific power loss, hotspot, or fire hazard.
- Microcracks and electrically inactive cell regions create the performance risk associated with some trails.
- Electroluminescence can reveal cell cracks and inactive areas that visual inspection cannot confirm.
- Infrared thermography can identify abnormal heating, but only under suitable irradiance and operating conditions.
- Cleaning may rule out surface dirt, biological residue, or hard-water marks, but it cannot repair a laminated defect.
What Are Solar Panel Snail Trails?
Solar panel snail trails are dark grey, brown, or black lines that appear over crystalline-silicon solar cells, commonly in branching or worm-like paths. The marks are called “snail trails” because their shape resembles a trail left by a snail, although the defect normally has no connection with living snails or surface contamination.
The marks typically form within the glass-encapsulant-cell stack. A surface wipe may leave the pattern unchanged because the discoloration is below the glass, often in or near the ethylene-vinyl acetate, or EVA, encapsulant. The appearance can overlap with other defects, including cell metallization discoloration, delamination, backsheet damage, busbar corrosion, and shadows from frame components.
A 2014 study titled A Defect Formation as Snail Trails in Photovoltaic Modules linked the phenomenon with interacting material and mechanical conditions rather than treating every dark line as one identical failure mode. That distinction matters: a visual label is a starting diagnosis, not a final engineering conclusion.
Are Solar Panel Snail Trails Only Cosmetic?
Solar panel snail trails are cosmetic when they produce no measurable inactive cell area, abnormal resistance, hotspot, or meaningful energy loss. They become a performance concern when the visible pattern accompanies cracked cell regions, corrosion of conductive fingers, electrical isolation, or localized heating.
The discoloration itself usually blocks less light than a substantial opaque obstruction. However, the mark can reveal a defect underneath it. The practical question is therefore not “How dark is the trail?” but “What electrical and thermal condition follows the trail?”
A module with extensive marks can still meet its power warranty, while a less dramatic crack may interrupt current flow in a cell and reduce output. Module age, cell layout, crack orientation, operating temperature, irradiance, and bypass-diode behavior all affect the result.
How Do Solar Panel Snail Trails Form?
Solar panel snail trails generally form through a combination of cell damage, moisture movement, encapsulant chemistry, and metallization corrosion. The commonly described pathway begins with a microcrack or vulnerable cell region, but published research does not justify claiming that every visible trail follows one universal chemical sequence.
The typical sequence is:
- Cell damage or manufacturing weakness: A silicon wafer develops a crack, weak edge, stressed region, or metallization defect during production, transport, installation, or service.
- Moisture and oxygen exposure: Water vapor reaches a susceptible region through edge pathways, polymer materials, imperfect seals, or existing laminate damage.
- Encapsulant chemistry: EVA can generate acidic decomposition products, including acetic acid, under moisture, heat, and aging conditions. The exact reaction rate depends on formulation and environment.
- Metallization attack: Corrosion can affect silver fingers or other conductive features on the cell surface, increasing the chance of current interruption.
- Visible deposition: Corrosion products or migrated materials create a dark pattern that becomes visible through the front glass.
The research literature supports a connection between snail trails, silver migration, encapsulant chemistry, and cell cracking, but the simplified claim that silver always becomes one named compound under sunlight is too absolute. Module construction and local chemistry vary.
Which Module Areas Do Trails Follow?
Trail position provides clues, but it does not identify the failure mechanism with certainty. A line crossing a cell may follow a crack, while a perimeter mark may indicate moisture movement, edge sealing weakness, or a different laminate defect.
| Visual pattern | Common location | Possible underlying condition | Diagnostic priority |
|---|---|---|---|
| Diagonal or branching line | Across one cell or several cells | Cell microcrack, metallization damage | EL imaging and power comparison |
| Parallel dark line | Beside a busbar or finger network | Contact corrosion or stress near conductive paths | EL, IV testing, close visual inspection |
| Perimeter discoloration | Near frame or laminate edge | Moisture ingress, edge seal, delamination | IR, laminate inspection, warranty review |
| Broad irregular stain | Between cells or over large areas | Encapsulant discoloration, delamination, contamination | Visual inspection and IR |
| Short isolated mark | Near a corner, clamp, or junction box | Handling stress or localized laminate damage | Mounting inspection and EL |
What Do Snail Trails Look Like Compared With Other Defects?
Snail trails are usually narrow, irregular lines beneath the glass, whereas ordinary dirt has a removable surface boundary and delamination often appears as bubbles, milky patches, or areas of optical separation. A trained inspector should compare the mark with cell geometry, busbars, frame edges, and known shading patterns.
| Condition | Surface cleaning changes appearance | Typical visual form | Main confirming test |
|---|---|---|---|
| Ordinary dust or bird residue | Yes | Soft-edged patch or streak | Cleaning and repeat photograph |
| Hard-water mineral deposit | Sometimes | White or translucent crust | Low-mineral rinse and inspection |
| Snail trail | No | Dark thin line or branching path | EL plus production review |
| Delamination | No | Bubble, haze, or lifted laminate | Visual inspection and IR |
| Cell microcrack without trail | No | Often invisible in daylight | EL imaging |
| Hotspot | No | May be invisible from ground | Infrared thermography |
Can Snail Trails Reduce Solar Panel Output?
Snail trails can reduce solar panel output when their associated crack or corrosion interrupts current collection, isolates part of a cell, increases resistance, or creates a bypass-diode-related mismatch. No universal 1%-2% or 9.1%-40% loss applies to every module, so output must be measured rather than inferred from trail area.
A crack can have little immediate effect if current still crosses the damaged region. A crack becomes more consequential when it separates electrically active portions of the cell or expands under thermal cycling. A module may then show lower current, lower fill factor, mismatch within a string, or intermittent behavior.
The practical evidence hierarchy is:
- Compare normalized energy yield with nearby unaffected modules.
- Check inverter and optimizer data for current or voltage divergence.
- Use IR to locate abnormal heating during stable operation.
- Use EL to map cracks and inactive cell regions.
- Perform an IV-curve test when a warranty or replacement decision requires quantified electrical evidence.
Annual degradation figures, often around 0.3%-0.8% for modern modules depending on product and study method, are not a diagnostic threshold by themselves. Weather, soiling, clipping, shading, snow, inverter limits, and sensor errors can produce larger short-term changes without cell failure.
Are Snail Trails a Fire Risk?
Snail trails alone do not establish a fire risk. Fire concern rises when a trail corresponds with a high-resistance connection, severe crack, junction-box issue, connector fault, or confirmed hotspot, which requires thermal or electrical evidence.
Thermal images must be interpreted carefully. A dark area can absorb more radiation than neighboring glass, and a temperature difference can result from uneven irradiance, wind, soiling, partial shading, or camera angle. IEC TS 62446-3 provides a framework for outdoor infrared inspection of photovoltaic systems, including the need to document operating and environmental conditions.
A confirmed hotspot, damaged junction box, melted connector, arcing sound, burning odor, or visible charring warrants prompt isolation by a qualified solar professional. Do not touch or disconnect energized DC equipment merely because a panel has cosmetic trails.
How Should You Test a Panel With Snail Trails?
Test solar panel snail trails in stages, starting with safe documentation and production review, then using infrared thermography or electroluminescence according to the suspected failure. A visual inspection is inexpensive, but it cannot determine whether a cell crack is electrically active.
| Test method | What it can reveal | Best operating condition | Typical cost range |
|---|---|---|---|
| Ground-level visual inspection | Pattern, location, glass and frame damage | Daylight, clean module surface | $0-$300 per visit |
| Inverter or optimizer data | String mismatch, current divergence, historical dips | At least 30-90 days of records | Usually included in monitoring |
| Infrared thermography | Hotspots, bypass-diode activity, connector heating | Clear conditions, stable load, strong sun | $150-$600 residential visit |
| Electroluminescence | Cell cracks, inactive regions, broken fingers | Module electrically biased in darkness | $100-$300 per module, typical |
| IV-curve tracing | Voc, Isc, fill factor, mismatch, power | Qualified technician and suitable irradiance | $250-$1,000 per system |
Costs vary by region, access, array size, travel, and whether the inspection covers one module or a full commercial site. The figures are typical field ranges, not universal prices.
When Is Electroluminescence Worth Paying For?
Electroluminescence is worth paying for when a warranty claim, replacement decision, or disputed performance issue depends on proving cell cracks or inactive regions. EL imaging makes electrically damaged areas visible, including defects that daylight photography cannot establish.
EL does not replace thermal testing. A cracked cell may appear in EL without producing a hotspot, while a thermal anomaly may come from a connector or bypass diode rather than a cell crack. For a residential claim, testing a representative sample may be economical; for a large site, an inspector may screen with IR before selecting modules for EL.
What Can Infrared Thermography Prove?
Infrared thermography can prove that a module, cell region, connector, or junction box is operating hotter than comparable components under the same conditions. It cannot, by itself, prove that a snail trail caused the anomaly or that a crack is present.
The inspection report should record irradiance, ambient temperature, wind, module orientation, camera model, image scale, operating current, and the location of each anomaly. A single image without those details is weak warranty evidence.
Can Cleaning Remove Solar Panel Snail Trails?
Cleaning cannot remove a true solar panel snail trail because the discoloration lies inside the laminate. Cleaning remains useful as a diagnostic step because it separates removable soiling and mineral residue from marks embedded below the glass.
Use manufacturer-approved cleaning procedures, soft non-abrasive tools, and water that will not leave damaging mineral deposits. Avoid walking on modules, abrasive pads, aggressive chemicals, and high-pressure washing. The International Electrotechnical Commission’s PV inspection standards emphasize documented inspection and electrical safety rather than cosmetic cleaning as a repair method.
A successful cleaning test changes the mark’s appearance or removes it from the glass. If the line remains in exactly the same position after safe cleaning, photograph the result and stop attempting to scrub it away. Repeated pressure cannot heal a cell crack and may damage coatings, seals, or glass.
Should Affected Modules Be Replaced?
Replace a module when testing confirms unacceptable power loss, a persistent hotspot, unsafe electrical damage, severe delamination, or a warranty-approved product defect. Do not replace every module solely because a faint trail is visible and system output remains within expected limits.
| Evidence found | Immediate decision | Follow-up interval | Replacement likelihood |
|---|---|---|---|
| Trail only, no output mismatch | Monitor and document | 6-12 months | Low |
| Trail plus EL crack, normal IR | Warranty assessment | 3-6 months | Medium |
| Trail plus measurable power loss | File claim and quantify loss | 30-90 days | High |
| Trail plus confirmed hotspot | Qualified isolation and urgent repair | Same day to 7 days | High |
| Trail plus connector or junction-box heating | Electrical fault response | Same day | High |
| Widespread trails with stable production | Portfolio sampling and trend analysis | Quarterly | Product-dependent |
Replacement also depends on module availability, electrical compatibility, roof access, labor, and the warranty’s remedy. A manufacturer may offer a replacement module with different current characteristics, creating string-design issues that an installer must check before substitution.
What If the Manufacturer Is Still in Business?
If the manufacturer remains active, submit a documented product or performance warranty claim before modifying the module. Include serial numbers, purchase records, installation date, photographs, monitoring exports, test reports, and the exact warranty clause that appears applicable.
A workmanship warranty may address visible laminate or material defects, while a power warranty addresses measured output after specified degradation. The distinction varies by contract. Never assume that a visible trail automatically qualifies under one category.
What If the Manufacturer Has Failed?
If the manufacturer no longer operates, collect independent evidence before replacing modules and check the installer, distributor, insurer, financier, and any extended warranty provider. A failed manufacturer can make a technically valid claim commercially worthless, so the evidence should support an engineering and financial decision.
For a small residential system, compare the cost of testing and labor with the cost of a compatible replacement. For a commercial array, calculate lost energy, truck rolls, spare inventory, and string redesign. A portfolio-level sampling plan may reveal whether the condition is isolated or systemic.
EVA, POE, or Glass-Glass: Which Construction Is More Resistant?
POE and glass-glass module designs generally provide stronger moisture resistance than conventional EVA with a polymer backsheet, but construction choice does not eliminate all cell cracks or field failures. EVA modules cost less and weigh less in many applications, while POE and glass-glass designs can increase material, handling, and structural requirements.
| Module construction | Moisture barrier | Typical relative cost | Typical weight implication | Main trade-off |
|---|---|---|---|---|
| EVA plus polymer backsheet | Moderate, dependent on seal and aging | Baseline, 100% | Lower, about 20-25 kg per module | Lower cost, greater moisture-aging exposure |
| EVA plus glass-glass | High on front and rear surfaces | About 105%-120% of baseline | Higher, often 25-35 kg | Better barrier, stronger racking demand |
| POE plus polymer backsheet | Higher than standard EVA | About 105%-115% | Similar to backsheet design | Better moisture resistance, formulation cost |
| POE plus glass-glass | Very high barrier potential | About 115%-130% | Highest, often 28-40 kg | Durability potential, handling and load penalties |
These percentages are typical market ranges, not a universal price list. POE does not literally guarantee “zero” degradation chemistry, and glass-glass construction does not eliminate transport damage, installation stress, junction-box failure, or cell cracking.
For humid, coastal, or high-voltage environments, moisture resistance may carry more weight than the initial price premium. For a roof with limited structural reserve, module mass and attachment loading may dominate the decision.
How Can Installers Prevent Snail Trails?
Installers reduce the risk of snail trails by preventing cell damage before and during installation, controlling clamp placement and torque, and recording module condition at delivery. Prevention is more reliable than post-installation cleaning because laminated cell damage is rarely field-repairable.
Use the following controls:
- Inspect pallet packaging before unloading and photograph crushed corners or shifted stacks.
- Lift modules by approved edges or handles, not by cables or junction boxes.
- Keep modules upright when the manufacturer specifies vertical transport and storage.
- Never walk, kneel, or place tools on module glass.
- Follow the manufacturer’s clamp zones and torque values, commonly specified in newton-metres on the installation manual.
- Prevent rails, clamps, and fasteners from contacting prohibited glass areas.
- Avoid stacking modules on uneven ground or placing debris between glass surfaces.
- Record serial numbers and photographs before installation.
- Use commissioning tests that establish baseline string voltage, current, and insulation condition.
A practitioner rule is simple: if a handling action would visibly flex the glass, it can load the cells beneath it. The absence of immediate visible damage is not evidence that the module survived transport or installation.
What Are the Most Common Diagnostic Mistakes?
The most common diagnostic mistake is treating the trail as the failure itself instead of a symptom that needs correlation with electrical and thermal evidence. Three errors repeatedly produce false conclusions.
- Using visual darkness as a power estimate: A larger or darker mark does not provide a reliable percentage loss. Cell layout and crack connectivity matter more than apparent color.
- Scanning under weak conditions: IR images taken near sunrise, in cloud, after cleaning, or under rapidly changing shade can create misleading temperature differences.
- Ignoring non-module causes: Inverter clipping, shading growth, optimizer faults, loose connectors, and soiling can mimic module underperformance.
A second practitioner rule concerns EL sampling. Testing one visibly affected module can prove a defect exists, but it may not represent an entire batch. Commercial owners should sample by model, production lot, installation area, and severity.
An honest limitation is that no remote article can determine whether a particular trail is electrically active. A serial-numbered inspection report, normalized production data, and qualified testing remain necessary for a replacement or safety decision.
What Action Plan Should Homeowners Follow?
Homeowners should document the marks, verify production, arrange targeted testing, and contact the installer or manufacturer before cleaning attempts or replacement. A stable monitoring record and a qualified inspection usually provide more useful evidence than a close-up photograph alone.
- Photograph each affected module with its serial number and date.
- Export 30-90 days of inverter or optimizer data.
- Compare affected and unaffected modules with similar orientation and shading.
- Arrange IR inspection if output differs or heating is suspected.
- Request EL or IV testing when the warranty claim needs proof of cell damage or power loss.
- Submit the evidence package to the installer and manufacturer.
- Keep the module in service only if the qualified assessment finds no safety issue and production remains acceptable.
Commercial operators should add aerial IR screening, string-level trend analysis, and defect mapping to scheduled operations and maintenance. A residential owner usually needs diagnosis of a small sample; a utility-scale owner needs prevalence, severity, and energy-loss estimates.
How Much Do Inspection and Replacement Decisions Cost?
A basic residential inspection typically costs $150-$600, while EL, IV tracing, roof access, or commercial drone work can increase the total to $1,000 or more. Module replacement cost depends heavily on labor and access, so the panel’s retail price alone is a poor estimate.
| Decision component | Typical residential range | Typical commercial range | Main cost driver |
|---|---|---|---|
| Visual inspection | $0-$300 | $300-$2,000 | Travel and array size |
| IR thermography | $150-$600 | $1,000-$10,000 | Roof access, drone permits, acreage |
| EL testing | $100-$300 per module | $75-$250 per module | Number tested and nighttime setup |
| Module replacement labor | $250-$900 per module | $100-$500 per module | Height, racking, wiring |
| Replacement module | $100-$400 | $80-$300 | Wattage, availability, compatibility |
The ranges are typical planning figures and should be confirmed locally. Warranty reimbursement may cover testing only if the manufacturer authorizes it in advance, so ask for written approval before commissioning specialized work.
The Bottom Line
Solar panel snail trails are cosmetic in appearance but potentially diagnostic of a performance problem. A visible trail does not justify automatic replacement, and the fixed loss figures sometimes repeated online cannot substitute for module-level evidence.
Start with photographs and normalized production data. Use infrared thermography to find abnormal heating, EL to identify cracks and inactive cell regions, and IV testing to quantify electrical impact. If testing confirms a hotspot, unsafe connection, or warranty-level power loss, pursue prompt repair or replacement. If testing finds no functional impact, retain the module, document the baseline, and monitor it on a defined schedule.
FAQ
Do snail trails mean my solar panels are defective?
Snail trails may indicate a manufacturing, handling, moisture, or metallization defect, but their appearance alone does not prove a warranty defect. The strongest case combines photographs with production data, EL evidence of cracking or inactive areas, IR evidence of heating, or an IV-curve result below the applicable specification.
How long do solar panel snail trails take to appear?
Snail trails can appear months or years after installation, depending on cell damage, moisture exposure, temperature cycling, encapsulant formulation, and module construction. A three-month-to-three-year window is often quoted in consumer material, but it is not a universal emergence timetable for every module or climate.
Can a cracked solar cell be repaired without replacing the panel?
A cracked solar cell normally cannot be repaired economically or reliably in the field because it is sealed inside the laminate. Some electrical faults outside the laminate, such as a connector or junction-box issue, may be repairable, but a qualified technician must distinguish those faults from cell damage.
Do glass-glass panels prevent snail trails?
Glass-glass panels can reduce moisture transmission through the rear of the module, particularly when paired with a moisture-resistant encapsulant such as POE. They cannot prevent all snail trails because transport impact, clamping stress, thermal cycling, cell defects, and junction-box problems can still damage a module.
Should I claim insurance for snail trails?
Insurance is usually relevant only when a covered event, such as hail, impact, storm damage, or handling damage, caused the module condition. A gradual material or manufacturing defect commonly belongs under a product or performance warranty instead, but the governing policy and warranty wording determine the available route.
Can snail trails spread across an entire solar array?
Snail trails do not spread like an organism. Similar marks across many modules may reflect a shared module design, production batch, environmental exposure, installation practice, or moisture condition. Batch-level sampling with visual mapping, IR, EL, and production analysis can distinguish a systemic pattern from isolated damage.